 EN
Home Skincare
Ideal for daily facial care routines, providing easy-to-use beauty solutions at home.

2026/10/26
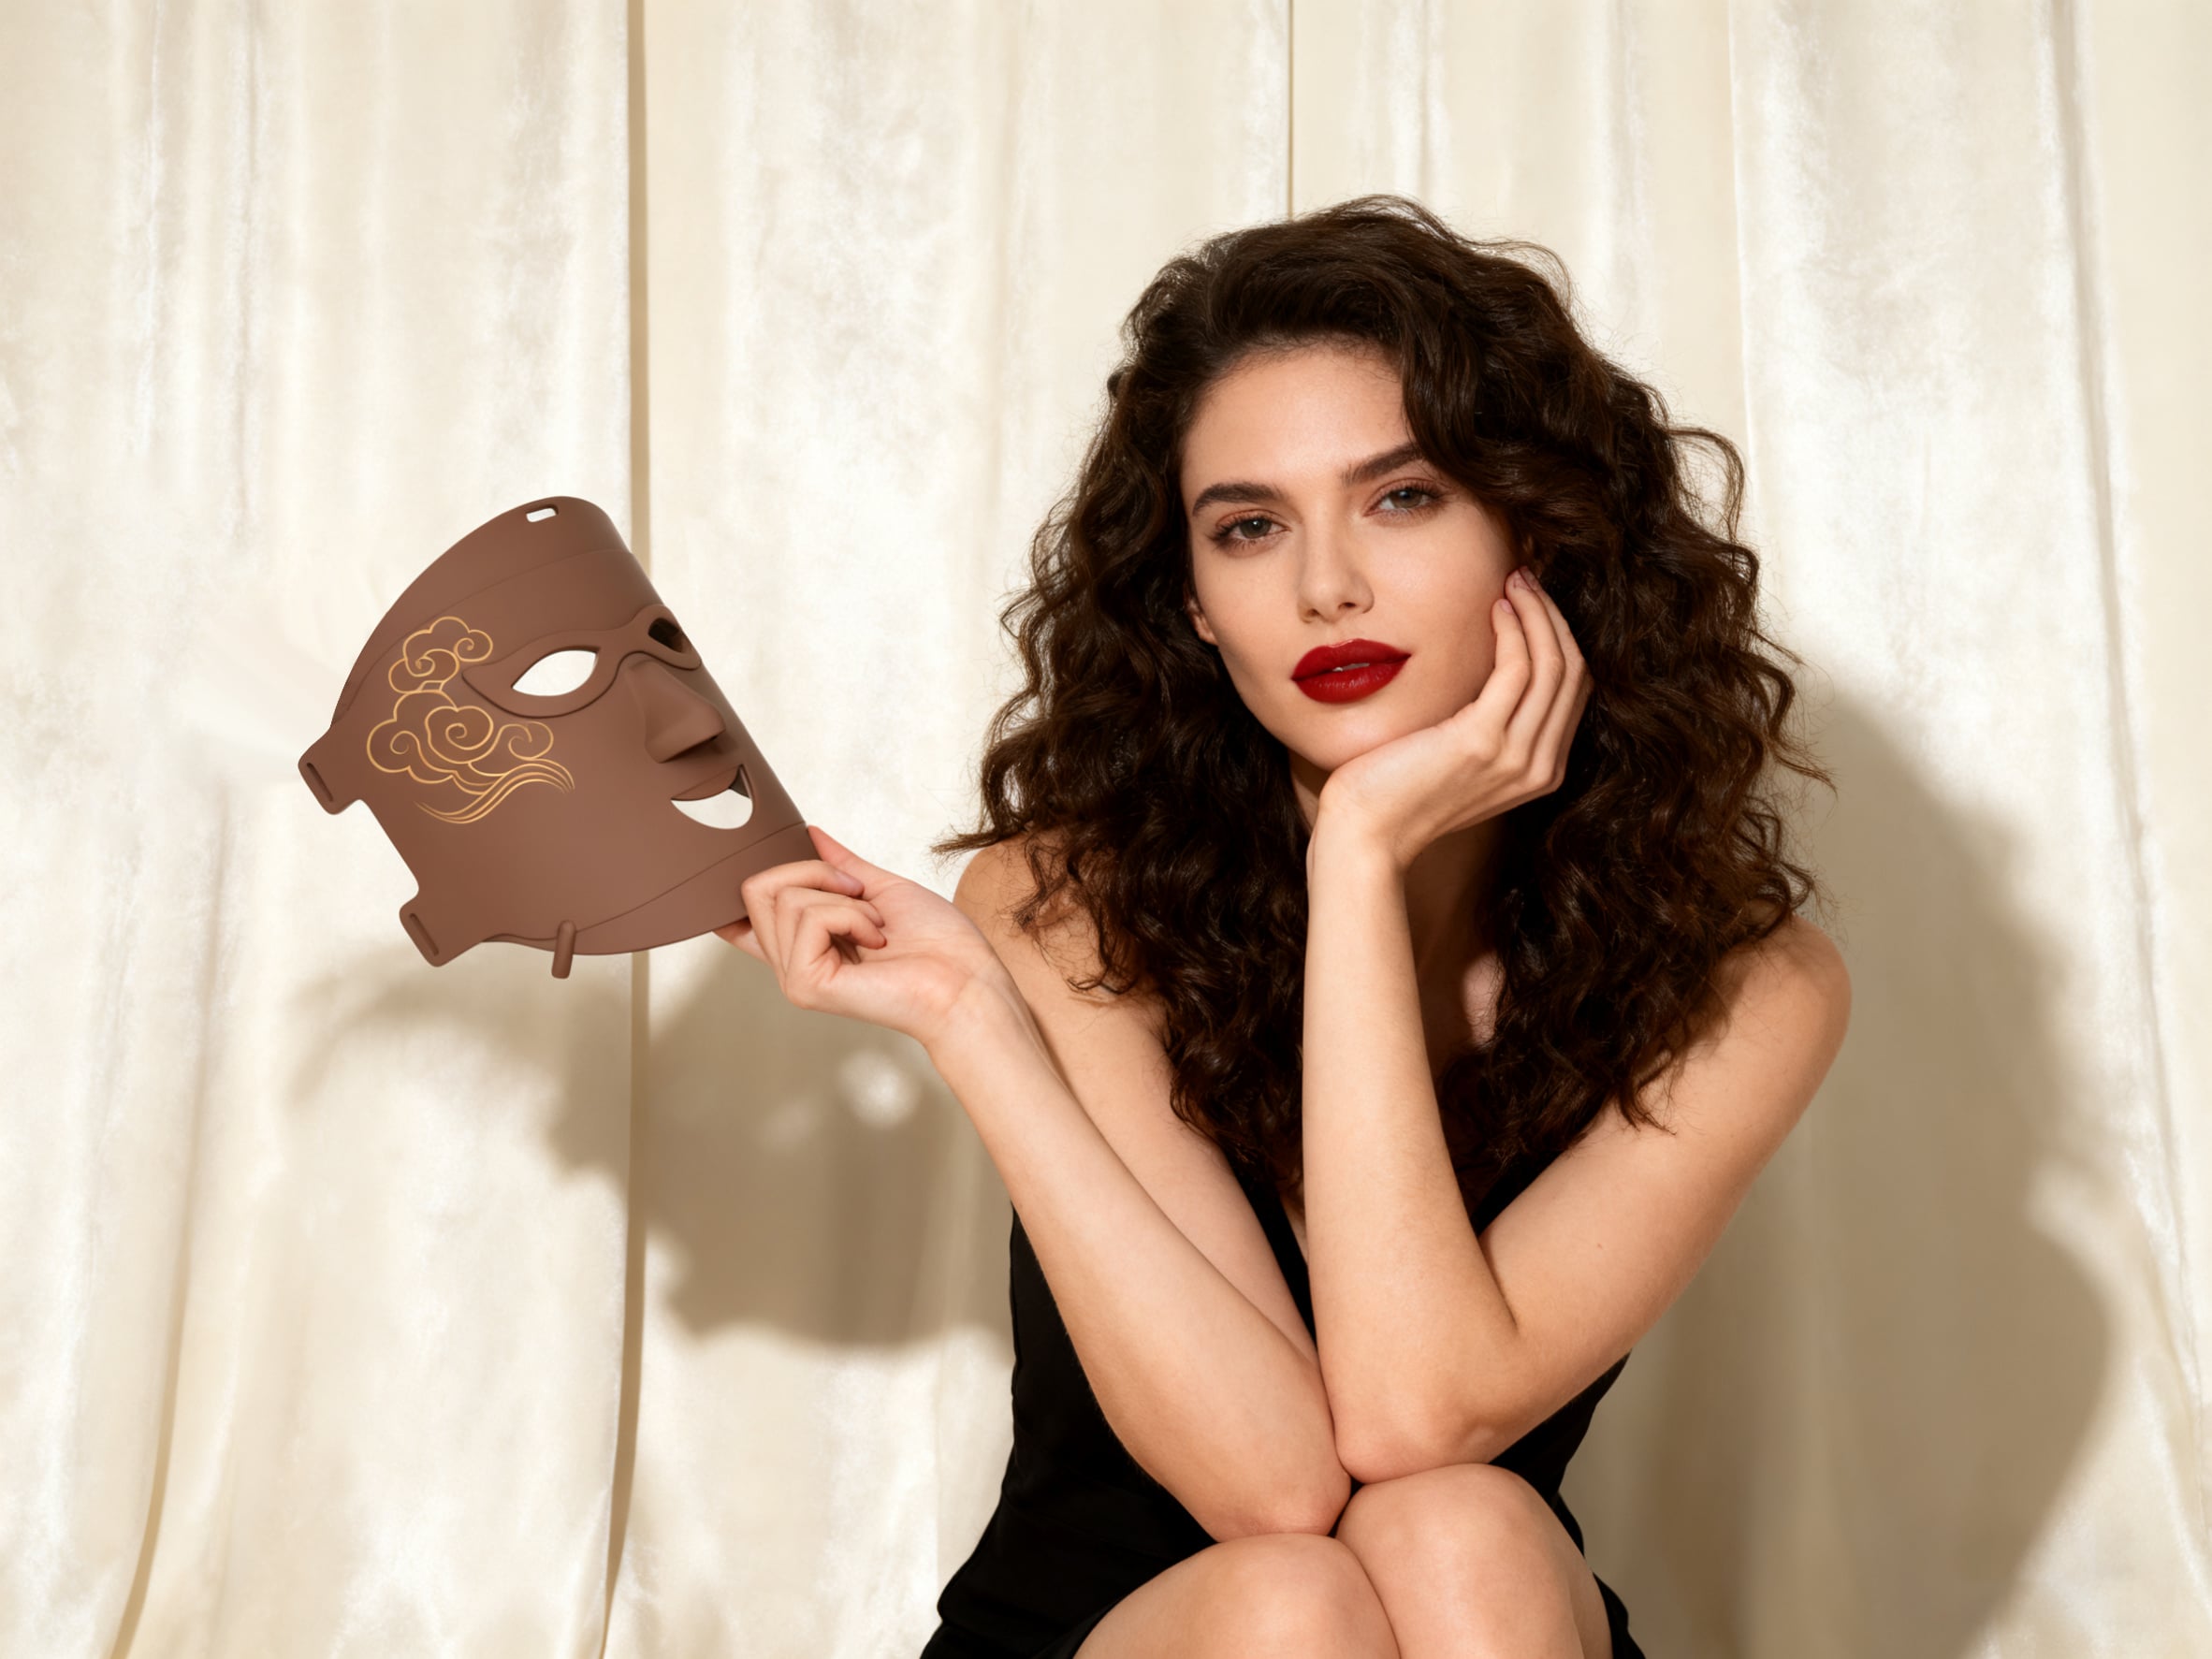
For a brand sourcing a silicone mask for LED skincare, the material is only the visible part of the decision. A flexible face form can look excellent in a sample yet become difficult to assemble, inconsistent in fit, or unreliable around embedded electronics when production scales. From an international buyer’s perspective, the useful question is not simply whether a factory can mold silicone. It is whether the factory controls the full chain: material traceability, mold design, curing, LED integration, inspection, and change control.
A well-made silicone mask is therefore a system rather than a single molded part. The following manufacturing checkpoints help brand teams turn an attractive concept into a repeatable product specification.
“Silicone” describes a family of materials, not one universal recipe. Before tooling begins, agree on the intended consumer use, skin-contact duration, cleaning method, color, feel, transparency requirements, and compatibility with LEDs, wiring, adhesives, and straps. These choices guide the selection of liquid silicone rubber (LSR), solid silicone rubber, pigments, and any post-cure process.
For a skin-contact silicone mask, the supplier should be able to identify the material grade, batch records, pigment or additive controls, and the documentation available from the material supplier. If a product will make medical claims or enter a regulated route, the evaluation plan needs to be defined for the finished device and its intended contact conditions. A material label alone is not a substitute for product-specific assessment.
There is a practical trade-off here. A softer formulation may improve facial conformity, while a firmer formulation can make handling and assembly easier. The right choice depends on the mask’s geometry, optical layout, and the brand’s target user experience—not on a generic claim that one hardness is universally preferable.
Facial masks commonly combine broad thin areas with eye, nose, and mouth openings. Those features place unusual demands on tooling. Gate location, flow length, cavity balance, vents, parting-line placement, and ejection all influence whether the molded silicone mask fills evenly and releases without deformation.
With LSR injection molding, two components are metered and mixed before the material enters a heated mold. That makes ratio control, air management, injection behavior, and curing conditions part of the quality plan. Poor venting can leave trapped air or incomplete edges; weak flash control can create rough trim work around sensitive facial cutouts; and inadequate support in a thin zone can lead to variation after demolding.
Ask the manufacturer to review the design for manufacturability before cutting production tooling. The review should identify critical dimensions, cosmetic surfaces, flash-sensitive edges, expected shrinkage validation, and the inspection method for each feature. It is cheaper to refine a gate or a locating feature at this stage than to compensate with handwork later.
For an LED skincare product, the silicone mask cannot be evaluated separately from the light engine. LED boards, flexible circuits, lenses or diffusers, connectors, and strain relief must remain correctly located while the mask flexes. The manufacturing plan should define how components are positioned before encapsulation or assembly, what prevents movement during curing, and how cable exits are protected from repeated bending.
One useful habit is to separate what the mold must control from what the assembly fixture must control. The mold can define the silicone geometry and cavities; a fixture may be needed to hold LED modules, align optical openings, or maintain cable routing during a secondary process. Clear datum strategy helps avoid a situation in which every part is individually “within tolerance” but the LEDs sit off-center relative to the facial openings.
Do not assume that a sealed appearance proves a durable assembly. Define pull, bend, illumination, and visual checks that reflect normal handling and cleaning. If adhesives, coatings, or inserts are used, validate their compatibility with the chosen silicone system and the product’s expected temperature and cleaning exposure.
Curing converts the uncured material into the finished elastomer, so time and temperature must be controlled as production parameters rather than treated as a background setting. The acceptable window depends on the selected formulation, geometry, tooling, and load. A process that works on a short pilot run may behave differently when cavities run continuously or when ambient conditions change.
For each silicone mask, document the approved mold temperature, cure time, mixing ratio, batch traceability, and any post-cure requirement. Then connect those records to inspection results. This creates a useful feedback loop: if softness, odor, color, fit, or surface finish shifts, the factory can investigate a defined process record instead of relying on memory.
It is also worth confirming how the supplier manages color matching and lot changes. Small pigment differences can be obvious on a large facial surface, and a material substitution can affect both appearance and assembly behavior. Changes should be reviewed and approved through a controlled process, especially after samples have been signed off.
A production inspection plan should include more than a quick visual check. Define incoming controls for silicone, electronic components, and packaging; in-process controls for molding and assembly; and finished-product checks that reflect how the mask is actually used.
Acceptance limits should be agreed in the specification, not improvised on the line. If a brand has a reference sample, it should be paired with measurable criteria; “match the approved sample” alone is too subjective for a high-volume silicone mask program.
Manufacturing readiness is not achieved when the first sample looks good. It is achieved when the supplier can make the same result repeatedly with documented controls. A sensible path is design review, tooling trial, engineering samples, a limited pilot, and only then a production release with agreed inspection records.
During each stage, record open issues such as edge flashing, LED alignment, odor, color, fit, or cable routing. Assign an owner, a corrective action, and a recheck method. This is less glamorous than an industrial-design review, but it protects the brand from recurring variability after launch.
An OEM and ODM partner can support product-function, appearance, and packaging customization across home beauty devices. For buyers, the productive conversation is to share the intended use, target market, desired light configuration, cleaning expectations, and brand requirements early. That lets the factory review process feasibility before cost and schedule become fixed.
| Focus | Recorded control |
|---|---|
| Material lot | Supplier batch release |
| Pigment | Color and additive verification |
| Mixing | Metering and mixing check |
| Mold cavity | Fill and venting review |
| Parting line | Flash acceptance limit |
| Thin zone | Thickness measurement plan |
| Facial opening | Cutout dimension check |
| Cure | Temperature and time record |
| LED cavity | Optical alignment verification |
| Circuit path | Cable-routing fixture control |
| Connector exit | Bend and strain-relief test |
| Surface | Contamination and edge inspection |
| Fit | Symmetry and recovery assessment |
| Assembly | Functional illumination check |
| Packaging | Identification and traceability check |
| Change | Engineering approval record |
Before approving a silicone mask project, ask for clear answers to these questions:
A disciplined silicone mask manufacturing program aligns material behavior, tool design, electronics integration, and quality verification from the first design review. When those controls are defined early, the factory and brand can focus on repeatability, not on correcting preventable issues after production begins.

2026/10/30
Discover why in-house mold development helps an RF beauty device manufacturer improve product consistency, iteration speed, tooling control, and production readiness.

2026/10/30
Learn how to verify an RF beauty device manufacturer's R&D and prototyping capabilities using practical engineering workflows and audit checklists.

2026/10/30
Learn what shapes MOQ when choosing an RF beauty device manufacturer and how to plan a lower-risk first order with balanced platform and customization.

2026/10/30
Use this RF beauty device manufacturer evaluation checklist to compare safety evidence, OEM and ODM capability, quality control, and launch readiness.

2026/10/30
See how technology makes beauty at home more guided, consistent, and informed—plus a practical checklist for choosing devices wisely.

2026/10/30
Explore how AI and smart devices shape the future of beauty with responsive routines, clear guidance, trustworthy design, and user-controlled care.

Ideal for daily facial care routines, providing easy-to-use beauty solutions at home.

Perfect for spas and salons’ frequent treatments, enhancing client experiences and results.

Supports dermatologists with advanced devices for professional skin therapy sessions.

Delivers innovative solutions for full-body massage and relaxation with home devices.

Features anti-aging technologies to help reduce wrinkles and stimulate skin vitality.

Specialized devices for safe and effective hair removal suitable for home or clinic use.

Our customers love the Perfect Idea beauty devices. Quality, packaging, and results are all outstanding. We saw increased repeat sales after adding their facial cleansers to our lineup. Their support team is responsive and reliable.

Perfect Idea brings innovation and reliability to home beauty appliances. Our collaboration introduced their massage tools to Japanese women, boosting customer satisfaction and growing our brand trust across the region.

We partnered with Shenzhen Perfect Idea Tech for their beauty equipment. The shipping was fast and every product matched our expectations. Their home-use massagers are especially popular with local salons and home users.

The stylish packaging and attractive design make Perfect Idea stand out. French consumers appreciate the easy instructions and visible results. Communication was efficient and orders always arrived on time.

Perfect Idea home use personal care devices have become a favorite with our clients. The beauty device line offers quality at a reasonable price, and technical training for our staff made onboarding easy.

We selected Perfect Idea for our beauty product portfolio and have seen very positive feedback from our customers. Products are easy to market online and the customer support is reliable and helpful.
